+8615674993216
 sales@forever-steels.com

 English
 العربية

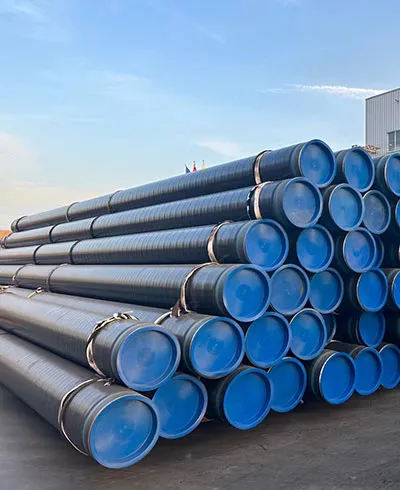
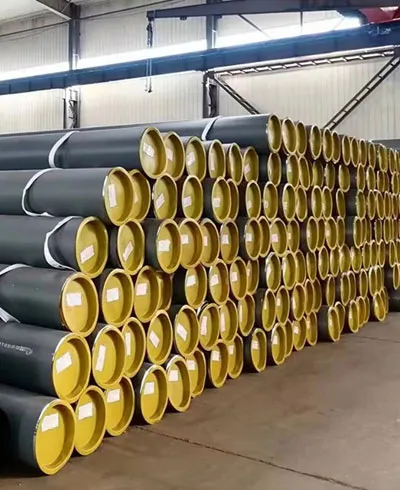
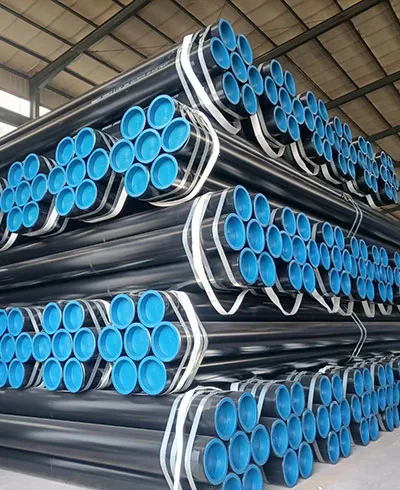
What should buyers check before coated steel pipe is shipped? Confirm surface-preparation records, specified coating thickness, adhesion or bond-test results, holiday-test coverage, closed repair and retest records, and protection during packing and loading. Results should identify the pipe or batch and the acceptance criteria in the approved coating specification. Appearance photographs alone cannot establish coating acceptance.
For a water-transmission order, 3LPE (three-layer polyethylene, also called 3PE) describes the external coating system. It does not specify the internal lining or establish drinking-water suitability for water-contact materials. The purchase specification should separately define the steel pipe, external 3LPE, internal lining and field-joint protection so each part has its own inspection and acceptance requirements.
| Part of the water-pipe package | Confirm before inspection | Record or responsibility to identify |
|---|---|---|
| Steel pipe | Standard, grade, OD, wall thickness, length and joint design | Producing mill, pipe identity and base-pipe inspection records |
| External 3LPE coating | Governing specification, thickness criteria, bond-test method, holiday-test procedure and permitted repairs | Coating applicator and pipe-linked inspection and repair results |
| Internal lining | Lining system, acceptance tests and applicable water-contact requirements | Lining applicator, inspection results and required suitability documentation |
| Cutbacks and field joints | Cutback dimensions, compatible joint-protection system and installation inspection plan | Who supplies, applies and accepts the field-joint protection; factory and site responsibilities |
| Packing and loading | Supports, separators, lifting method and end protection | Final condition check and agreed loading records |
Use the coating standard and edition named in the project specification. ISO 21809-1:2018 covers external three-layer PE and PP coatings for petroleum and natural-gas pipeline systems; it should not be assumed to define a complete water-pipe package. The AWWA standards list separately identifies exterior polyolefin coatings and other coating or lining systems. Confirm which requirements the water project actually adopts.
For 3LPE pre-shipment release, check individual thickness readings, the specified bond-test results, holiday-test settings and coverage, and the acceptance of every repair. Use project-approved test methods and limits; there is no single voltage or adhesion threshold to apply to every coated pipe order.
Coating protects the steel surface from direct contact with moisture, soil, chemicals or the outdoor environment. If the coating is too thin, poorly bonded or damaged during handling, corrosion can start before the pipe is installed.
This is especially important for coated pipe orders used in underground pipelines, water transmission, piling, marine-adjacent projects, oil and gas service, outdoor storage or long-distance shipment.
· Coating thickness below requirement
· Uneven coating near the weld seam or pipe end
· Peeling or delamination
· Pinholes or holidays not visible to the eye
· Scratches caused by handling or bundling
· Poor repair quality
· Rust at cutback or bevel areas
· Damage during loading or transport
· Missing inspection or repair records
|
Inspection Item |
What It Confirms |
Buyer Concern |
|
Surface preparation |
Steel surface is clean and suitable for coating |
Rust, oil, dust, mill scale or poor blasting can weaken adhesion |
|
Coating thickness |
Coating meets minimum or specified thickness |
Thin areas may reduce corrosion protection |
|
Adhesion test |
Coating is properly bonded to steel |
Weak bonding may cause peeling or delamination |
|
Holiday test |
Coating has no discontinuities or exposed steel points |
Pinholes may become corrosion starting points |
|
Visual inspection |
Surface condition is acceptable |
Scratches, bubbles, cracks, sagging or poor finish |
|
Repair inspection |
Damage was repaired correctly |
Poor repair may fail after shipment or installation |
|
End protection |
Pipe ends, bevels and cutback areas are controlled |
Ends are common rust and damage areas |
|
Packing inspection |
Coating is protected during handling and transport |
Bad packing can damage good coating before arrival |
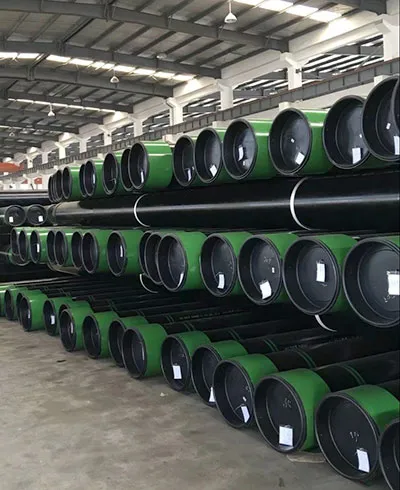
For anti-corrosion coating orders such as 3PE coated steel pipe or FBE coated steel pipe, these inspection items should be confirmed before shipment, not after the goods are already loaded.
Many coating failures begin before the coating is applied. If the steel surface is not properly cleaned, blasted or prepared, the coating may look acceptable at first but fail later.
|
Surface Issue |
Possible Result |
|
Rust or mill scale left on surface |
Poor coating bond and early underfilm corrosion |
|
Oil or grease contamination |
Local adhesion failure or fish-eye defects |
|
Moisture before coating |
Blistering, weak adhesion or coating defects |
|
Poor blasting profile |
Coating may not anchor properly to the steel surface |
|
Dust after blasting |
Weak bond between coating and substrate |
Coating thickness is one of the most important inspection items because it directly affects corrosion protection. If the coating is too thin, service life may be reduced. If it is too uneven, weak points may appear even when the average thickness looks acceptable.
Thickness is usually measured with a dry film thickness gauge or coating thickness meter. The order should define the required thickness, acceptance method and measurement frequency.
|
Area |
Why It Should Be Checked |
|
Main pipe body |
Confirms general coating uniformity |
|
Weld seam area |
Raised welds may lead to thinner or uneven coating |
|
Pipe ends |
Cutting, beveling and handling can affect coating at ends |
|
Repaired areas |
Repair material must meet required thickness |
|
Support or contact points |
Coating can be damaged by racks, lifting tools or bundling |
|
Cutback area |
End cutback must match project and field joint requirements |
For coated welded steel pipe orders, the base pipe and coating requirements should be reviewed together. A rough weld seam, sharp edge or poor pipe end condition can affect coating quality even if the coating material itself is correct.
Adhesion means how well the coating bonds to the steel surface. Good adhesion depends on surface preparation, coating material, application temperature, curing condition and handling after coating.
A coating can have enough thickness but still fail if it does not bond properly. Depending on the coating system and specification, adhesion may be checked by cross-cut test, pull-off test, peel test or another project-approved method.
|
Adhesion Problem |
Possible Cause |
Buyer Risk |
|
Peeling from steel surface |
Poor surface preparation or contamination |
Coating may fail during handling or service |
|
Lifting near damaged area |
Weak bond around the defect |
Damage can spread beyond the original scratch |
|
Delamination |
Process error, moisture or poor curing |
Large coating areas may separate from steel |
|
Poor repair adhesion |
Repair area not cleaned or prepared correctly |
Repaired area may fail before installation |
A holiday test detects discontinuities in the coating. These may include pinholes, cracks, thin spots or tiny exposed steel points that cannot always be seen visually.
The test voltage must match coating type and coating thickness. Too low a voltage may miss defects. Too high a voltage may damage the coating.
|
Holiday Test Item |
Buyer Should Confirm |
|
Test requirement |
Is holiday testing required by the order or project specification? |
|
Test voltage |
Does the voltage match coating type and thickness? |
|
Test coverage |
Is the full pipe body checked or only selected areas? |
|
Defect marking |
Are detected holidays clearly marked before repair? |
|
Repair and retest |
Are repaired areas tested again? |
|
Report |
Is a holiday test record provided before shipment? |
Coating repair is common, especially on large-diameter pipes, heavy pipes, long pipe lengths and export shipments. The issue is not whether repair exists. The issue is whether repair is controlled.
· Pipe number or bundle reference
· Repair location
· Type of damage
· Surface preparation before repair
· Repair material used
· Repaired thickness
· Holiday test after repair
· Final acceptance result
· Photos before and after repair if required
|
Repair Situation |
What Buyers Should Check |
|
Small scratch |
Was exposed steel cleaned before repair? |
|
Pinholes found by holiday test |
Were all holidays marked, repaired and retested? |
|
Coating peel-off |
Was weak surrounding coating removed before repair? |
|
Pipe end damage |
Was end protection restored before packing? |
|
Large repair area |
Was repair accepted according to project specification? |
Technical tests are essential, but visual inspection remains useful because many practical shipment problems are visible.
· Scratches or cuts
· Peeling or cracking
· Bubbles or blisters
· Uneven coating appearance
· Rust at pipe ends
· Damage around lifting points
· Coating damage caused by stacking
· Poorly patched repair areas
· Contamination on coating surface
· Broken end caps or damaged protection
A coating may pass inspection after production but still be damaged before delivery if packing and handling are not controlled.
· Whether pipes have suitable separators or padding
· Whether direct steel-to-steel contact is avoided
· Whether lifting belts are used properly
· Whether pipe ends are protected
· Whether coated surfaces are dragged or scratched
· Whether bundles are too tight or poorly supported
· Whether rainwater can be trapped inside wrapping
· Whether loading photos show coating condition clearly
· Coating type
· Surface preparation grade
· Required coating thickness
· Thickness measurement method
· Adhesion test requirement
· Holiday test requirement
· Repair standard
· Pipe end cutback requirement
· End protection method
· Packing method
· Third-party inspection requirement
· Required inspection reports and photos
Pipe coating inspection should not stop at appearance. A smooth coated surface does not automatically prove the coating is qualified.
For buyers, the most important inspection items are surface preparation, coating thickness, adhesion, holiday test result, repair record, end protection and packing condition. These items show whether the coating can actually protect the pipe after shipment and handling.
At Forever Steels, coated steel pipe orders can be supported with coating requirement review, thickness inspection, adhesion and holiday test coordination, repair documentation, packing inspection and shipment photo records before delivery.
Continue with these closely related Forever Steel technical resources:
• ISO 21809-2:2026 — Single-Layer Fusion-Bonded Epoxy Coatings — International Organization for Standardization.
• ASTM G62-23 — Holiday Detection in Pipeline Coatings — ASTM International.
• ISO 21809-11:2019 — Coatings for In-Field Application, Repairs and Rehabilitation — International Organization for Standardization.
• Holiday Testing: What It Is and Why It Is Needed — Materials Performance, Association for Materials Protection and Performance.
• Coating Application on Pipelines — Association for Materials Protection and Performance.
• Cathodic Disbondment Testing Under Realistic Field Conditions — Pipeline Research Council International; research performed with Case Western Reserve University.
Coated pipe should be released from recorded acceptance results, not from appearance photographs alone. The dossier needs to connect each inspection result to the coating system, batch or pipe identity, test location, instrument, acceptance criteria, repair action and retest status.
The following record map helps a buyer see whether a reported result is complete enough for shipment release.
| Inspection item | Record should show | Release question |
| Surface preparation | Cleanliness, profile and specified contamination checks | Was the substrate accepted before coating? |
| Thickness | Gauge identification, calibration, locations and individual readings | Do readings meet the specified minimum and range? |
| Adhesion or bond test | Method, frequency, condition and result | Was the correct test used for this coating system? |
| Holiday detection | Detector type, test voltage basis, coverage and findings | Was the full required surface tested after handling? |
| Repair and retest | Defect location, repair material, cure, thickness and holiday retest | Is every repair closed with an accepted retest? |
| Loading condition | Final visual check, separators, lifting method and end protection | Was accepted coating protected through loading? |
A report that states only “passed” cannot show whether the correct voltage, measurement frequency or repair method was used. The approved ITP and coating procedure should define those details before production, while the final dossier demonstrates that the agreed controls were followed.
For 3PE coated steel pipe and FBE coated steel pipe orders, Forever Steel can align the requested record list with the quotation and pre-shipment release file. Project-specific acceptance values still come from the governing coating specification and approved procedure.